Belt Monitoring

Belt Tear Switches

Industrial conveyor safety devices designed to detect belt tearing or rupture conditions and provide an electrical signal for warning or conveyor tripping applications.

Belt Tear DetectionDamage MonitoringConveyor Protection
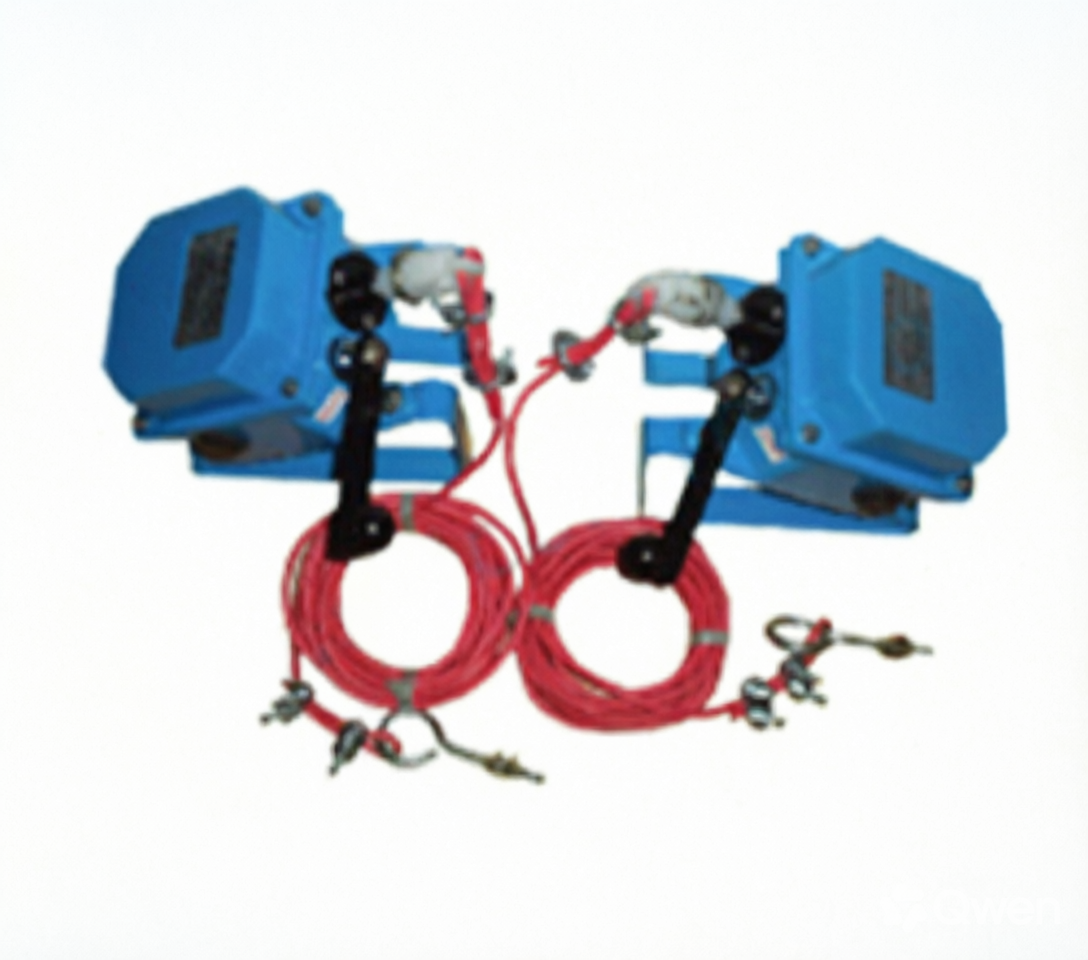
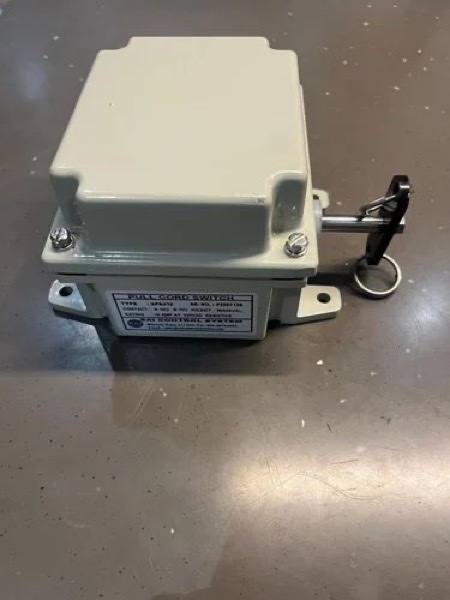
Industrial belt tear switch for conveyor belt damage detection
  • Conveyor Protection
  • Belt Monitoring
  • Industrial Use

Belt Tear Switches

Belt Tear Switches are industrial conveyor safety devices designed to detect belt tearing or rupture conditions and provide an electrical signal for warning or conveyor tripping applications.

Monitoring units are installed along the conveyor with sensing ropes positioned across the belt-monitoring area. If the conveyor belt tears, projecting or torn belt material can displace the sensing rope and actuate the monitoring switch.

The switch provides potential-free electrical contacts that can be connected to a suitable warning, alarm, or conveyor tripping circuit. After operation, the switch is manually reset and the sensing rope must be returned to its correct operating position before restarting the conveyor.

Belt Tear DetectionManual ResetIP65 Protection2NO + 2NC Contacts
Call us now08043873299Speak to our conveyor safety specialist

How Belt Tear Switches Work

Operation Sequence

  • Monitoring units are installed in an inclined position in the direction of conveyor belt movement.
  • Sensing ropes are connected between the monitoring units.
  • During normal operation, the sensing rope remains in its normal position.
  • If the belt develops a serious tear, projecting portions of the damaged belt can push the cross-connected sensing rope.
  • Movement of the rope actuates the Belt Tear Switch and provides a warning or conveyor-trip signal.
  • The switch requires manual reset after operation, and the sensing rope must be manually repositioned before conveyor restart.

Key Features

  • Conveyor belt tear detection
  • Designed for conveyor protection applications
  • Rope-operated sensing arrangement
  • Potential-free switching contacts
  • Manual reset mechanism
  • Heavy-duty industrial construction
  • IP65 degree of protection
  • Cast aluminium enclosure
  • 2NO + 2NC contact arrangement

Technical Specifications

Key Specifications

ProductBelt Tear Switch
ApplicationConveyor belt tear detection and protection
EnclosureCast Aluminium
Degree of ProtectionIP65
ActuationTorn-belt material moving the sensing rope
ResetManual Reset
Contact Arrangement2NO + 2NC
Contact Rating10 A Resistive @ 110 / 240 V AC, 50 Hz
Sensing MethodCross-connected sensing rope
Sensing Rope LengthTwo ropes, each approximately 5 metres long

Set Components

  • Pair of monitoring units
  • Mounting frame
  • Two sensing ropes
  • Each sensing rope approximately 5 metres long
  • 8 rope clamps
  • 2 hooks

Control System Integration

  • Conveyor control panel
  • PLC input
  • Alarm system
  • Warning indication
  • Trip circuit
  • Safety/control relay system

Applications

  • Industrial belt conveyors
  • Bulk material handling systems
  • Conveyor belt protection
  • Conveyor tear detection
  • Material handling plants
  • Mining and mineral handling conveyors
  • Conveyor warning and tripping systems

Installation Note

The monitoring units should be positioned appropriately along the conveyor system and installed in the direction of belt movement.

The sensing ropes are cut to the required installation length and positioned so that abnormal torn-belt material can displace the rope and operate the switch.

Verify model-specific dimensions, exact mounting requirements, certifications and application-specific electrical requirements from the official manufacturer datasheet before publishing them as guaranteed specifications.

Interested in Belt Tear Switch for Conveyor Belt Damage Detection?

Get in touch for application support, pricing and availability.

Get Instant Quote